India: Improving FDM 3D Printing Through Process Parameter Optimization
In ‘Process Parameter Optimization for FDM 3D Printer,’ researchers from India discuss varying ways to improve popular fabrication processes, exploring basic parameter settings like density, layer height, and shell thickness—and how they affect mechanical properties like surface roughness, hardness, and tensile strength of 3D printed parts.
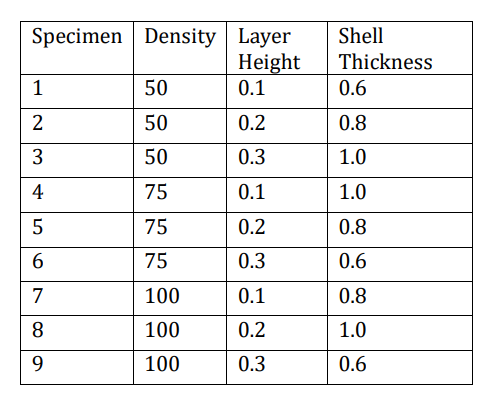
Specimen printing parameter variations
Using 1.75mm PLA as their material of choice, the scientists used an I3D Minds 3D printer for testing, SOLIDWORKS for design, and CURA for slicing. The I3D Minds offers a build volume of 190x190x180 mm and nozzle diameter of 0.4 mm, and automated setup and manufacturing.
Design samples were opened in CURA, and varying parameters were set:
- Different layer heights – 0.1mm, 02mm, and 0.3mm
- Fill densities – 50%, 75%, 100%
- Shell thickness – 0.6mm, 0.8mm, 1.0mm
Sample files were converted into G-Code, and then sent to the 3D printer:
“The nozzle was maintained a temperature of 215 ºC for the extrusion of the PLA material and the build plate was maintained at 60 ºC,” stated the authors. “The printer prints the layer through the nozzle print head onto bed, one layer by layer, from bottom to top, and the same test setup was used for all specimens. The post hardening was observed to investigate the unconditional effect of printing parameters on physical and mechanical properties of the printed specimens.”

CAD modeling
The researchers also touched on common issues such as how to prevent issues due to common errors that may occur at the .stl file stage, often easily averted with ‘repair’ fixes in the original model.
“Generally, STLs that have been produced from a model obtained through 3D scanning often have more of these errors,” said the authors. “This is due to how 3D scanning works—as it is often by point to point acquisition, reconstruction will include errors in most cases.”
Printing a ‘slightly oversized version’ of the object is also suggested for greater precision in parts.
In discussing the Taguchi method, created by Dr. Genichi Taguchi, one of the leaders in parameter design, the researchers suggest using an orthogonal array for balanced results. This balance also means that each part can be evaluated on its own because each one is equal.
“On the basis of varying different parameters in different levels a Design of Experiments was carried out which can be used for preparation of specimens for optimization of 3D printed products for different parameters of 3D printing,” concluded the researchers. “Testing machines are selected for testing mechanical properties such as tensile strength, hardness and surface roughness of 3D printed specimens.”
While many may refer to 3D printing as magical, plenty of brainpower—in labs around the world—still goes into thinking of ways to refine nearly all methods. In FDM printing, researchers explore ways to improve layer adhesion, review how products like sensors are created, and discuss popular types of composites. Find out more about how scientists are improving parameter optimization here. What do you think of this news? Let us know your thoughts! Join the discussion of this and other 3D printing topics at 3DPrintBoard.com.
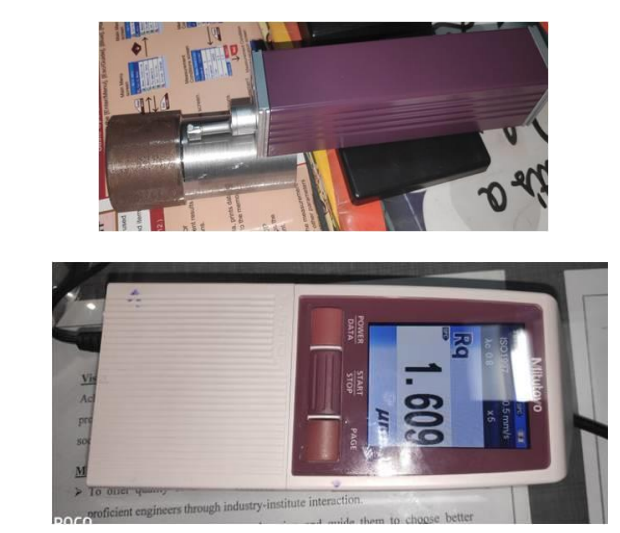
Surface roughness test
Subscribe to Our Email Newsletter
Stay up-to-date on all the latest news from the 3D printing industry and receive information and offers from third party vendors.
Print Services
Upload your 3D Models and get them printed quickly and efficiently.



You May Also Like
Printing Money Episode 42: Q2 2026 Public Markets 3D Printing Earnings Analysis with Troy Jensen, Cantor
Welcome to Printing Money Episode 42. Troy Jensen (Managing Director, Cantor) returns, joining Danny Piper (Managing Partner, NewCap) to review Q2 2026 publicly traded 3DP/AM company earnings reports. Troy’s quarterly...
3DPOD 314: Debinding, Sintering, and Metal Binder Jetting with Stefan Joens, Elnik Systems and DSH Technologies
Stefan Joens of Elnik Systems sells ovens. Their debind and sintering equipment powers a lot of high-volume binder jet and MIM production. We learn about Elnik and its origins. But...
The Frankenservice Part 1: Print the Rainbow
So far, most service bureaus and manufacturing companies stick to what they know. Not only for OCD reasons, but gleaming lines of identical LPBF machines are also arrayed on impossibly...
3DPOD 313: Patient-Specific 3D Printing with Ruben Wauthle, Amnovis
Ruben Wauthle studied at Leuven University at a very serendipitous time. Through working with pioneering additive professors and surgeons, he entered into a specialty that was emerging. He joined pioneering...